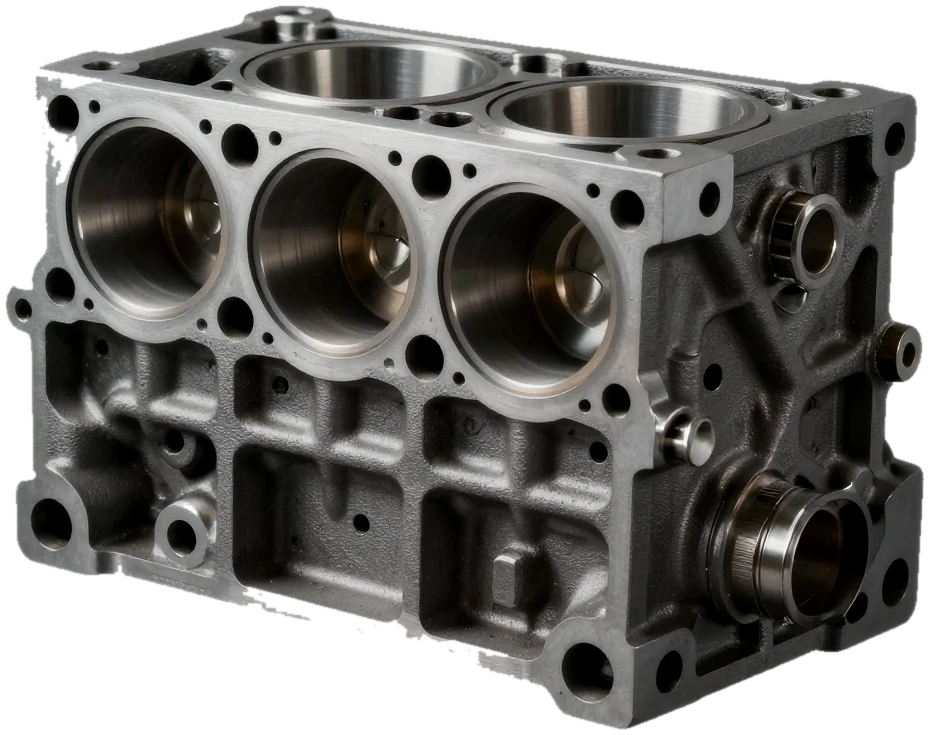
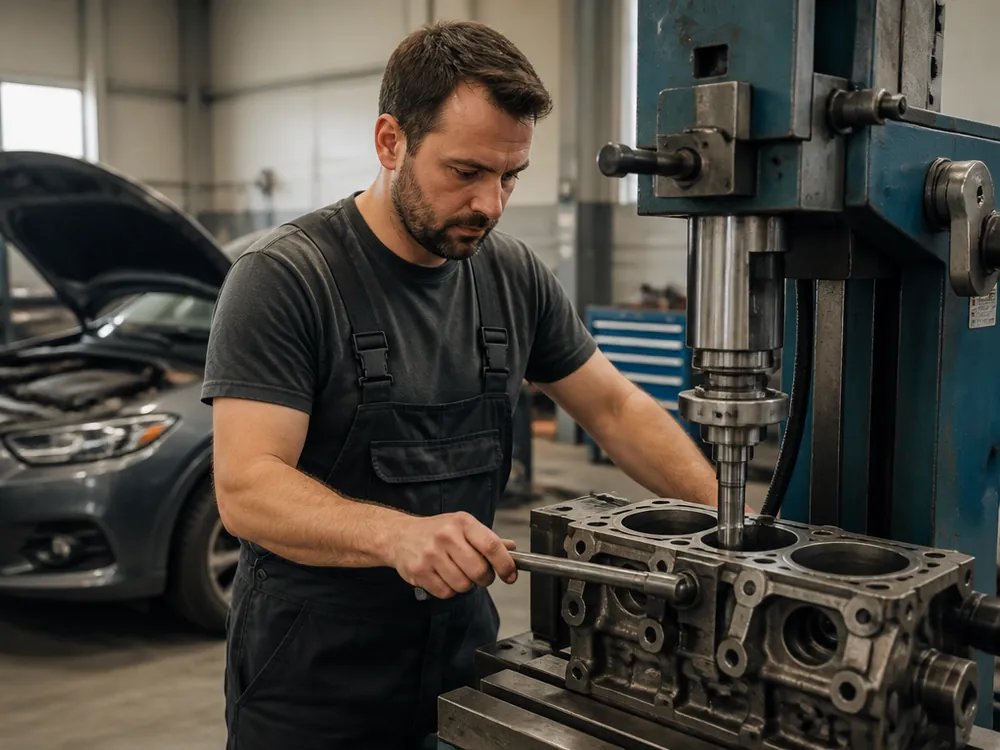
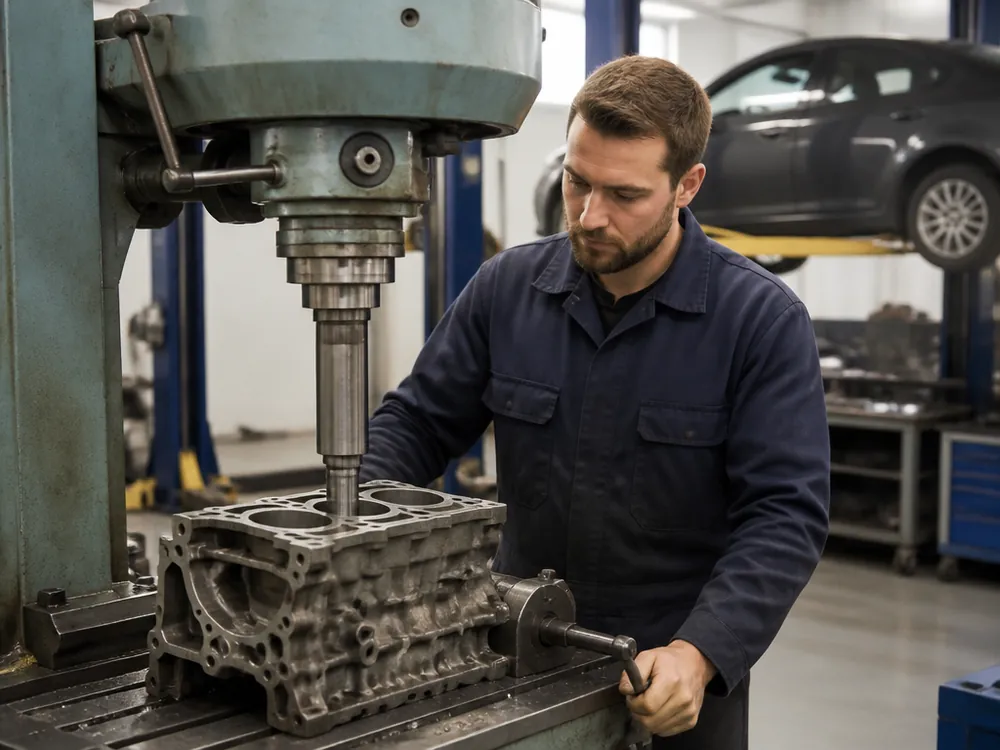
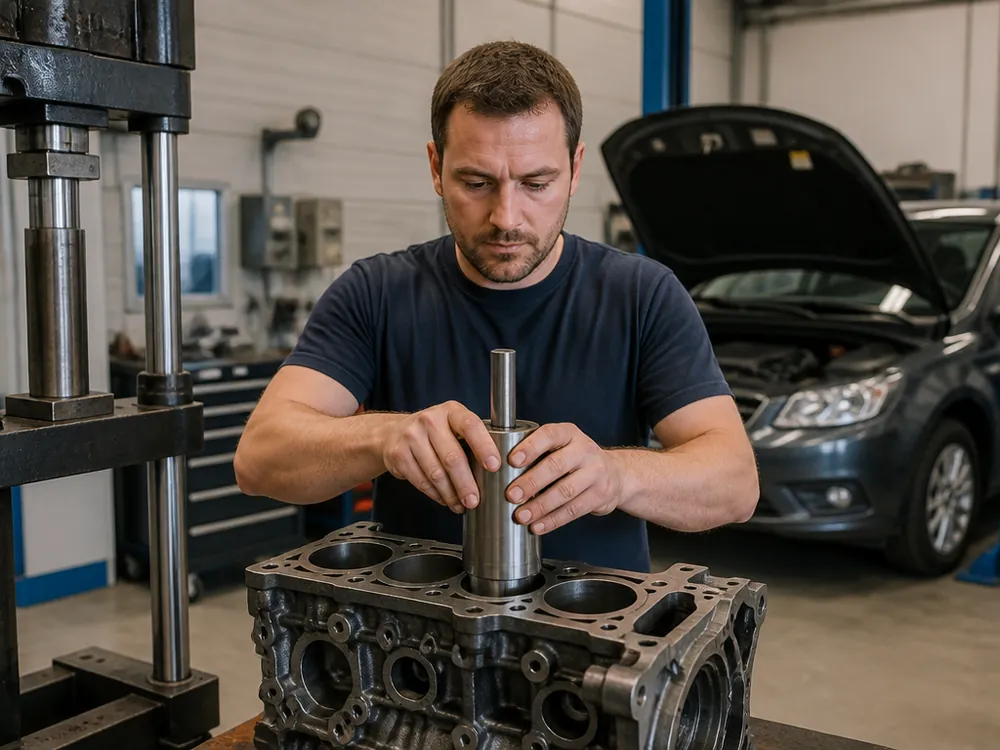
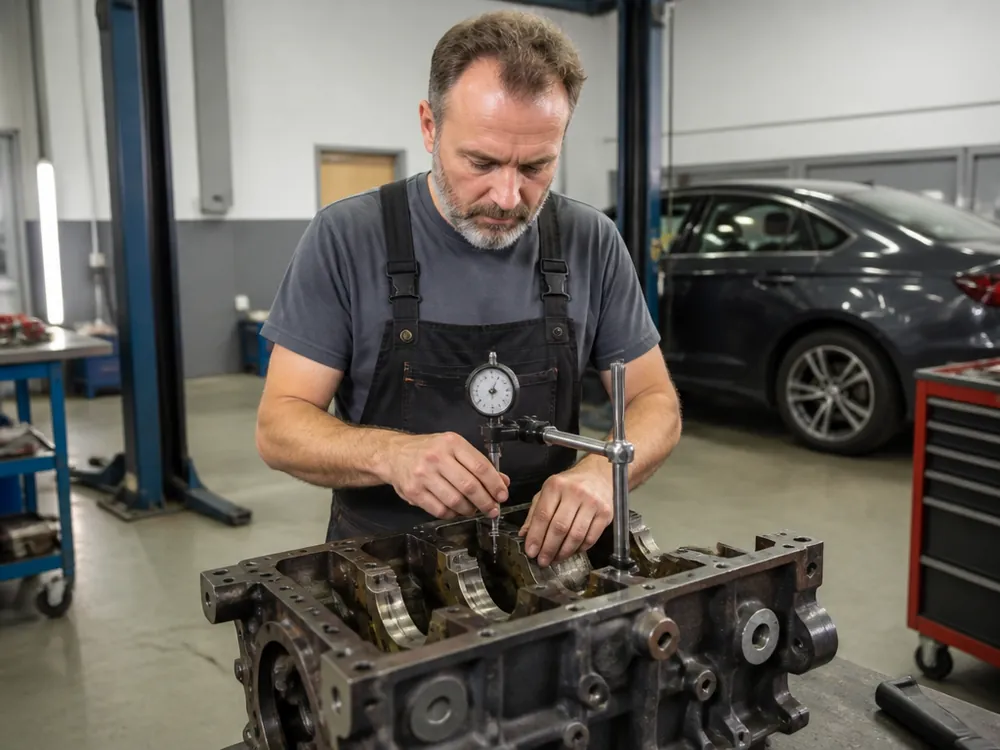
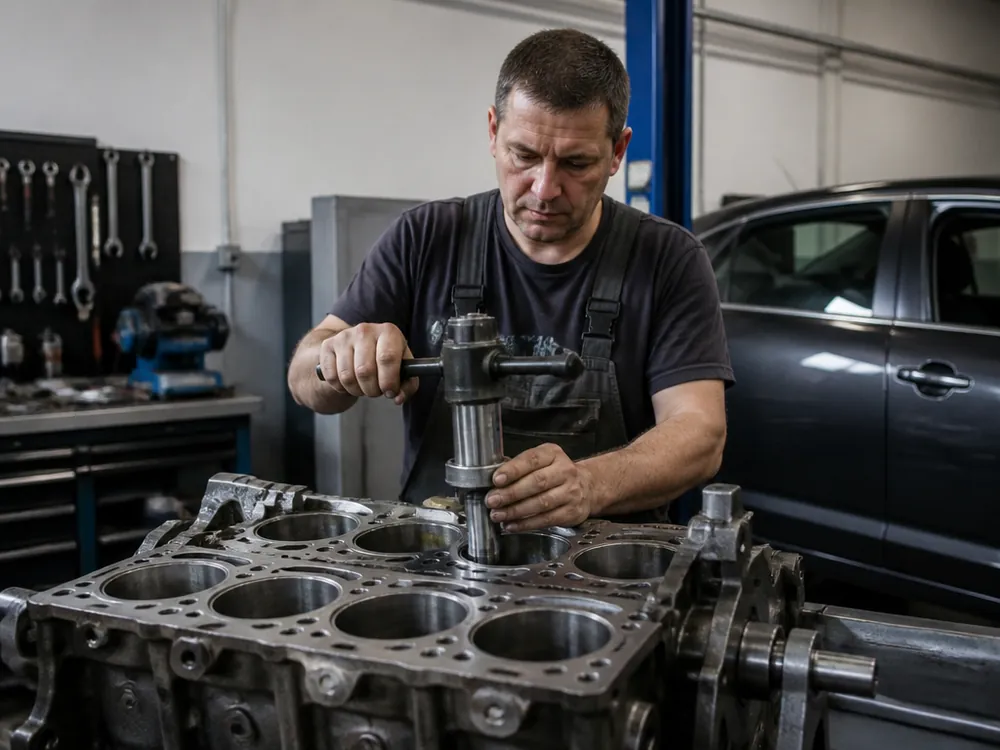
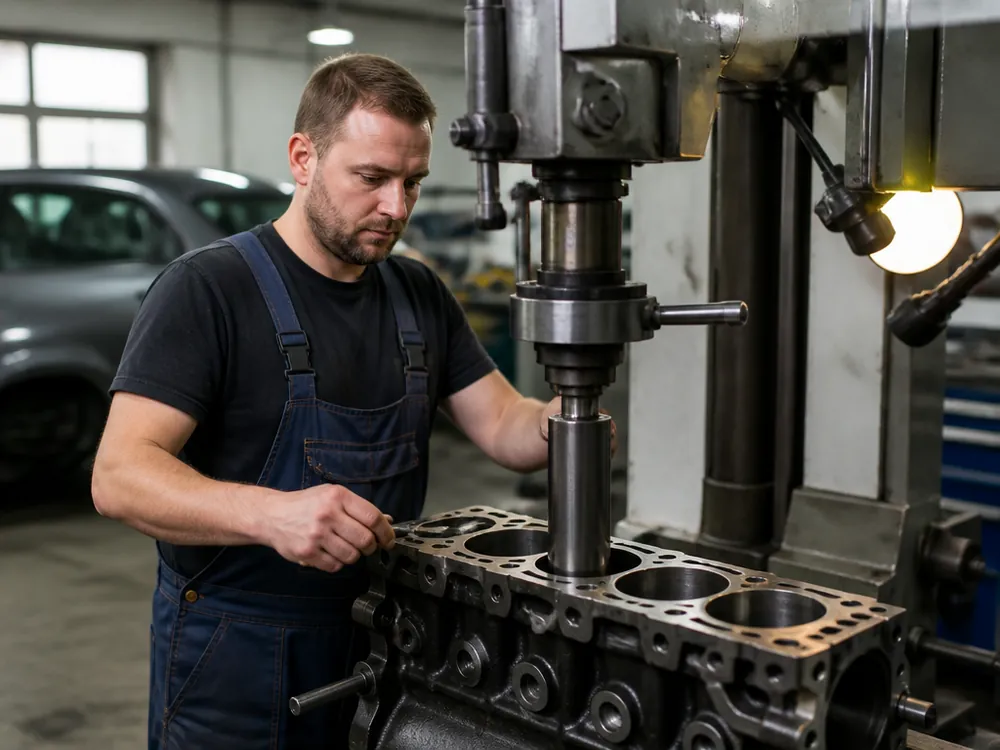
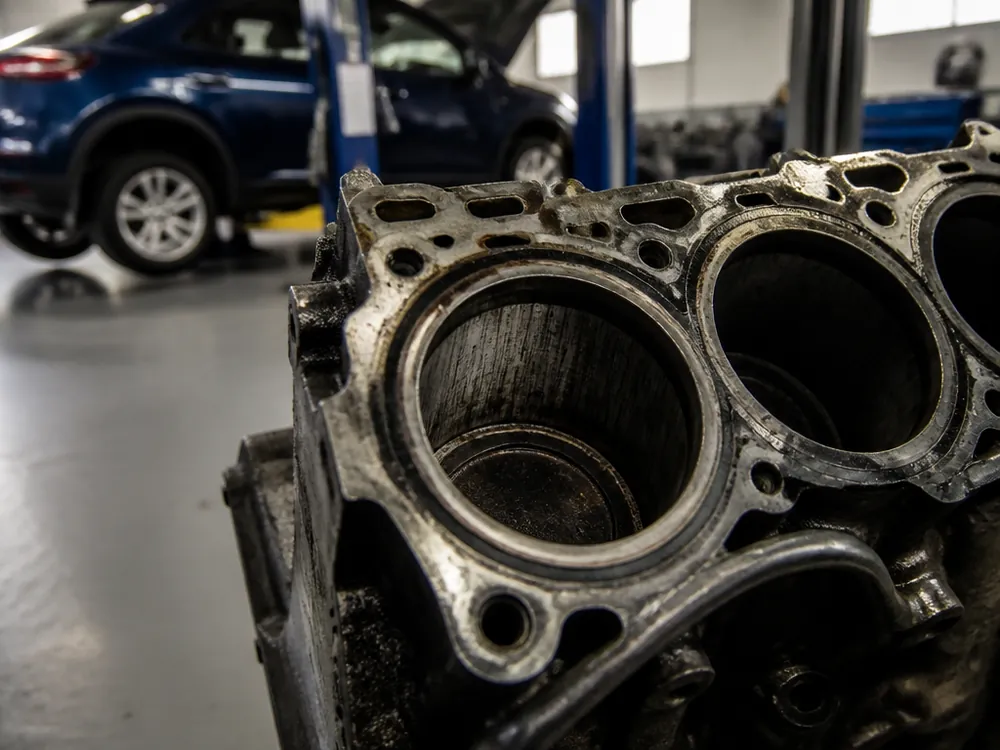
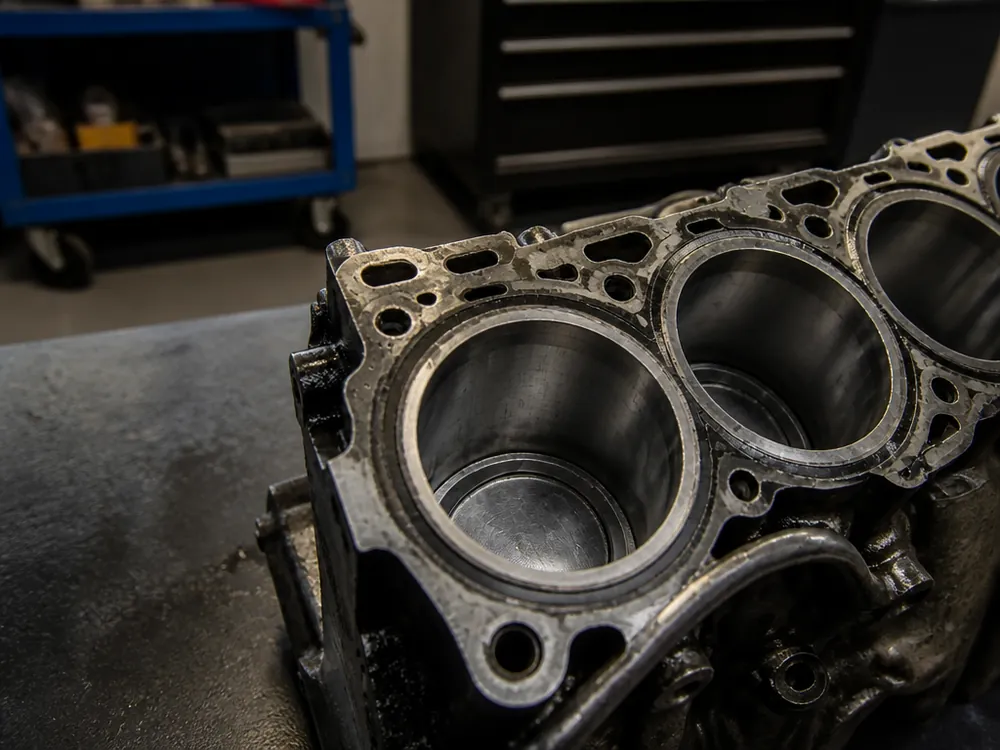
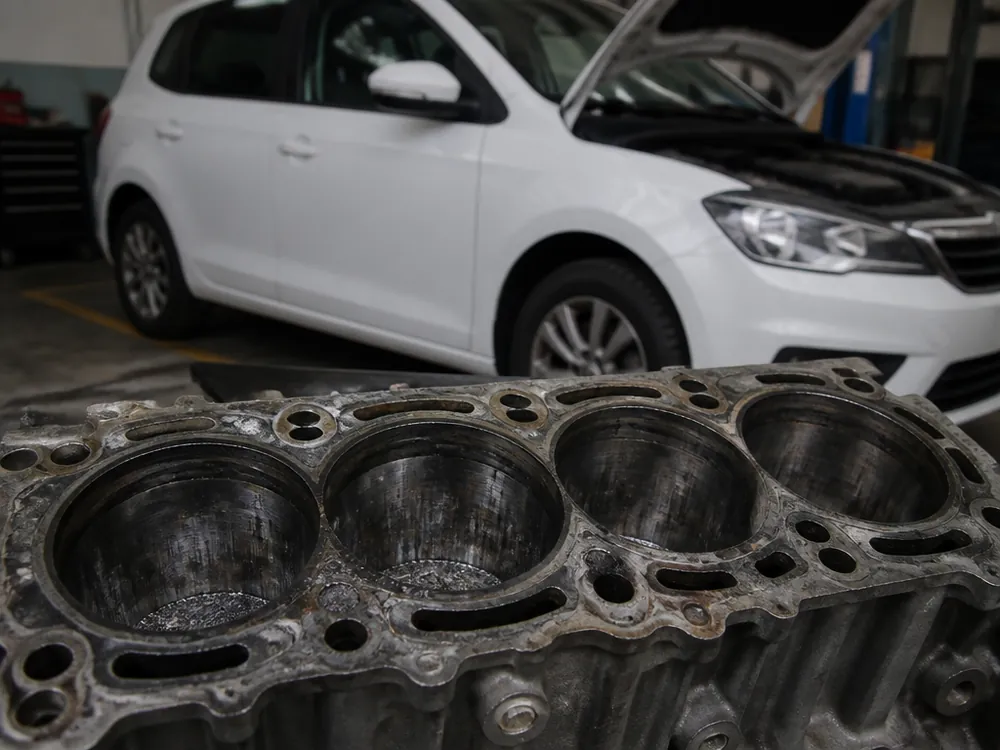
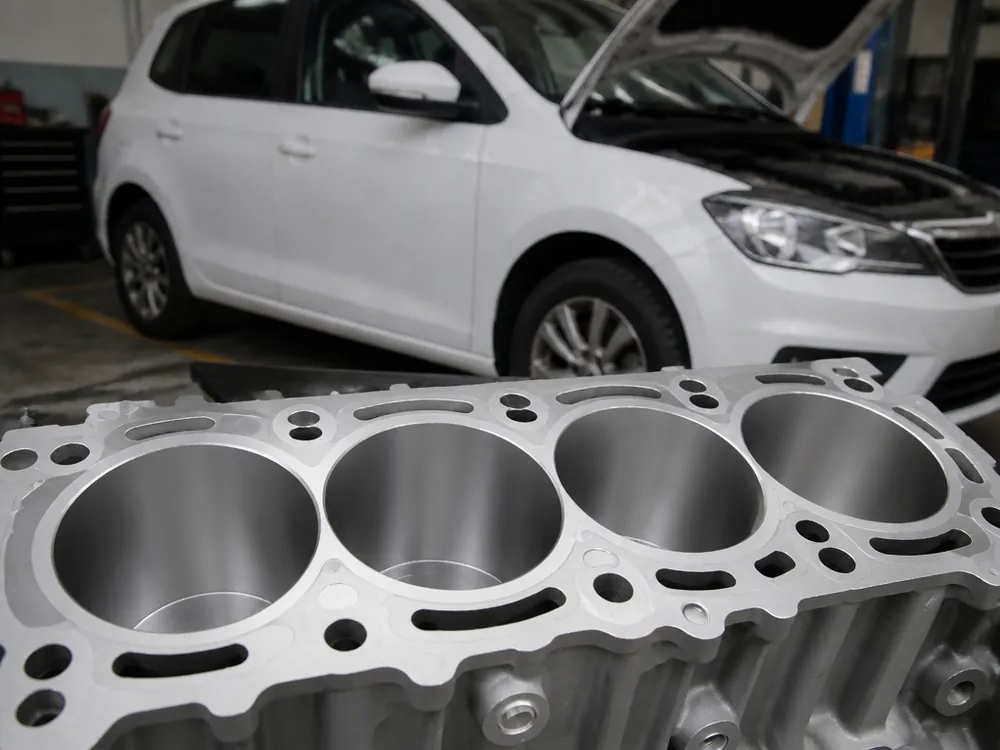
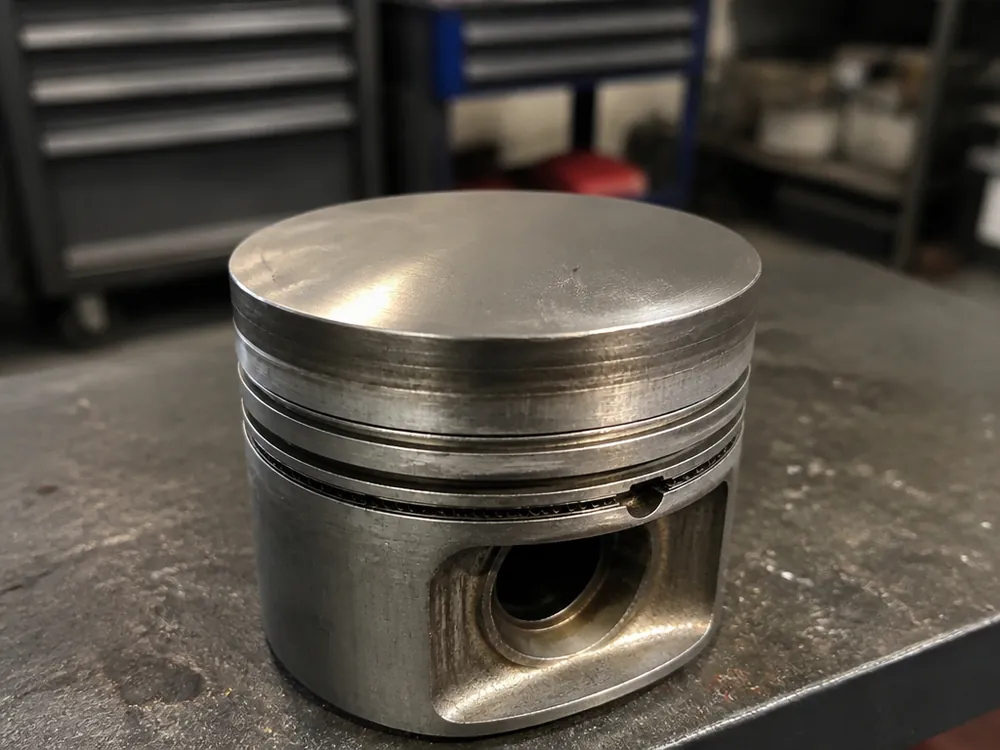
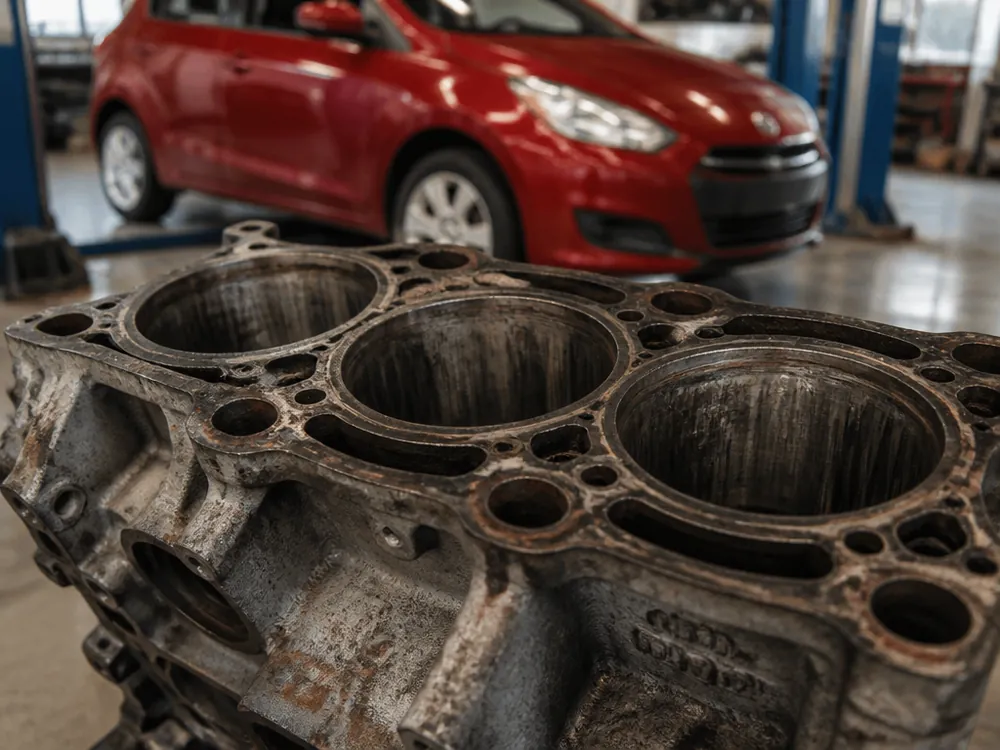
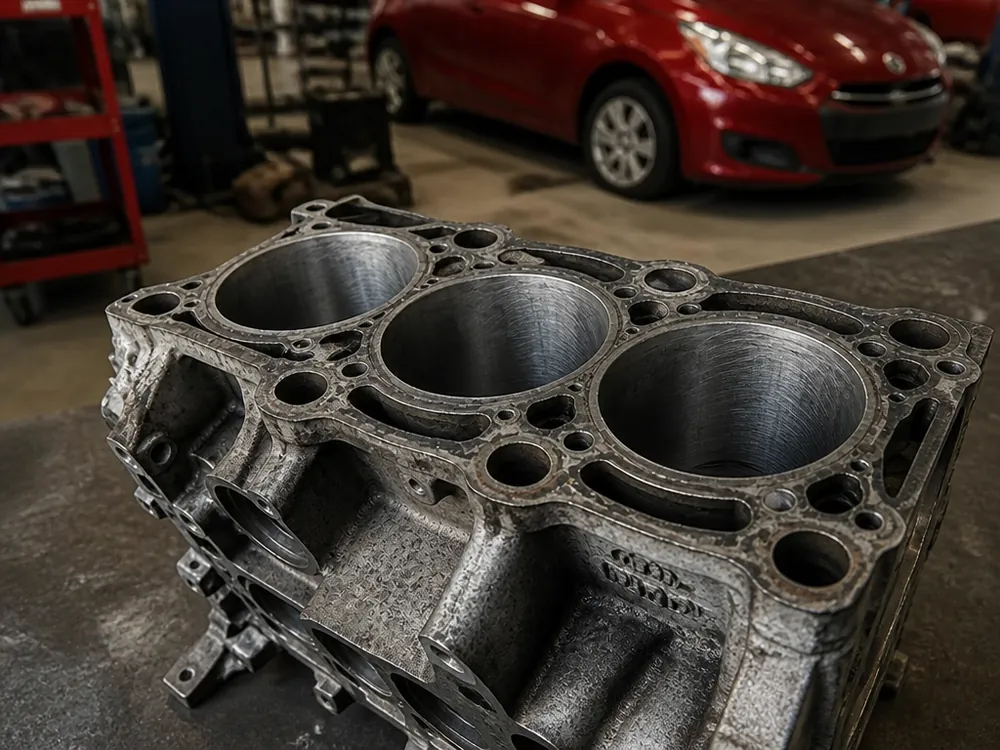
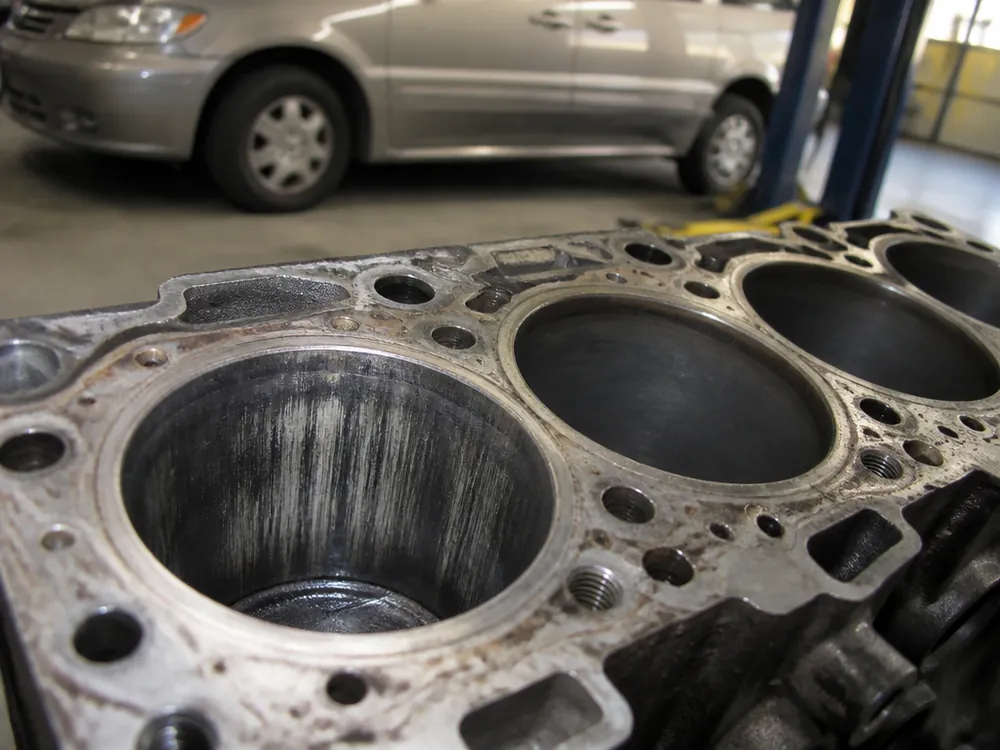
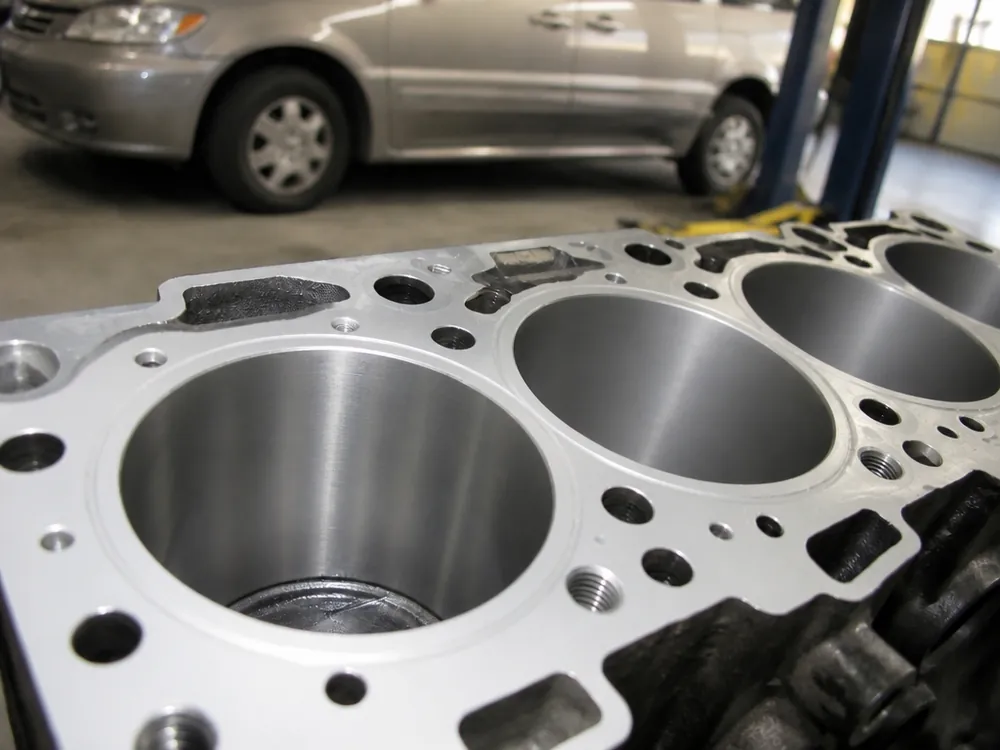
We restore the cylinder block to factory geometry: boring to repair or nominal size, honing, surface polishing. We use professional equipment and ensure accuracy up to 0.01 mm. Warranty on work — 12 months. Cost calculation after diagnostics — free of charge.
Precision boring to repair size, honing and washing. Prices are for typical operations.
Service
Duration
Warranty
Price
Cylinder block diagnostics, measurement and defect detection
1–2 hours
12 mo
from 5 000 ₸
Cylinder block washing before boring
1 hour
12 mo
from 3 000 ₸
Mounting the block on the boring machine, alignment
1 hour
12 mo
from 4 000 ₸
Boring of one cylinder (cast iron, up to 0.5 mm)
1–2 hours / cylinder
12 mo
from 7 000 ₸
Boring of one cylinder (aluminum, with sleeving)
2–3 hours / cylinder
12 mo
from 10 000 ₸
Honing of one cylinder
1 hour / cylinder
12 mo
from 5 000 ₸
V6 block boring (all cylinders)
1–2 days
12 mo
from 45 000 ₸
Inline-four block boring (all cylinders)
1 day
12 mo
from 35 000 ₸
Boring with sleeve installation (complete set)
2–3 days
12 mo
from 60 000 ₸
Milling of the block surface (mating surface)
3–4 hours
12 mo
from 8 000 ₸
Express boring (within the day)
4–6 hours
12 mo
from 25 000 ₸ (surcharge)
On-site block diagnostics with cylinder head removal
2–3 hours
12 mo
from 8 000 ₸
Block boring with crankshaft main bore repair
2–3 days
12 mo
from 50 000 ₸
Block boring with bearing replacement (related)
1–2 days
12 mo
from 15 000 ₸
Block boring for oversized piston (1st repair)
1 day
12 mo
from 30 000 ₸
Block boring for 2nd and 3rd repair size
1–2 days
12 mo
from 38 000 ₸
Sealing and pressure testing of the block after boring
2–3 hours
12 mo
from 6 000 ₸
Control measurement and issue of the report
1 hour
12 mo
from 4 000 ₸
Prices are indicated excluding the cost of spare parts and consumables. The exact cost depends on the condition of the block and the engine type — please check after defect detection. Warranty periods — see the page «Warranty»
06
Advantages of cylinder block boring at CARGID
Warranty.
Every promise — backed by a number or a document: work order, photos, removed parts.
12MO
warranty on labor — the term is stated in the work order.
Block diagnostics
12-month warranty
Free inspection
01
Runout check
Before boring, we check the seats and deformation of the bedplate. Without this, any repair will lead to oil consumption and knocking.
02
Boring for 3 sizes
We measure wear with a bore gauge and select the repair piston. We bore exactly to the required size, not «by eye».
03
Sleeving with 0.05 mm interference
We press the sleeve with interference so it does not turn. This saves the block in case of deep scuffs and cracks.
04
12-month warranty
We give a year on cylinder geometry provided break-in is observed. If an ellipse or scuff appears, we will redo it at our own expense.
07
How engine restoration works at our shop
Steps.
We explain how cylinder block boring is carried out in our auto service — from request to finished engine.
01
Block inspection
You leave a request, we book you for a convenient time and give preliminary recommendations. A specialist inspects the block, measures the cylinders and assesses the possibility of boring.
request on WhatsApp
02
Approval of work
We discuss the diagnostic results, state the exact cost and timeframes before starting work.
inspection and diagnostics
03
Block boring
On a boring machine we remove the minimum layer of metal to eliminate wear and out-of-roundness.
estimate before work starts
04
Honing
We create precise cylinder geometry and the correct microprofile for better oil retention.
work to factory procedure
05
Washing and inspection
We thoroughly wash the block from chips and carry out control measurements of all seats.
result check
06
Assembly
We transfer the block for assembly with new pistons and rings, selecting them according to tolerances. You receive a finished block and a warranty for the performed boring work.
Car service in Almaty. We reply on WhatsApp and by phone.
3 000 ₸Cylinder block washing before boring
10 · Useful
Cylinder block boring in Almaty without rework or uneven tone
Author: Роман Вернерgeneral car repair technician, 13 years of experience
Published Updated
Cylinder block boring at CARGID in Almaty means restoring cylinder geometry to the required repair size with honing and a control measurement. We start with an inspection and a written estimate, and begin repairs only after the client agrees. The boring comes with a 12-month warranty, and the timeline and terms are recorded in the work order.
Which boring do you need, the block or the cylinder head
Clients often come in with a ready-made request but mix up two different units and two different jobs: cylinder head boring and block machining are not the same thing. We separate the concepts so you bring your car in with the right request and don't pay for extra work.
How block machining differs from head restoration
Block: machining the cylinders inside the engine body — we remove a layer of metal from the walls for an oversize piston.
Cylinder head: restoring the head — resurfacing the deck, replacing valve seats and guide bushings.
Different units: the block holds the pistons and crankshaft, the head closes the combustion chambers from above.
Different tooling: cylinders are machined on a boring machine with axial alignment, the head on milling equipment.
Different result: after boring the cylinders the thermal clearance changes, after the head it's the sealing and valve seating.
Common sign of trouble: if the technician didn't clarify which unit needs machining, the estimate will be put together by eye with extra line items.
How to tell from the symptom which unit needs repair
Intake: our service advisor first records the symptom and repair history rather than naming a job over the phone.
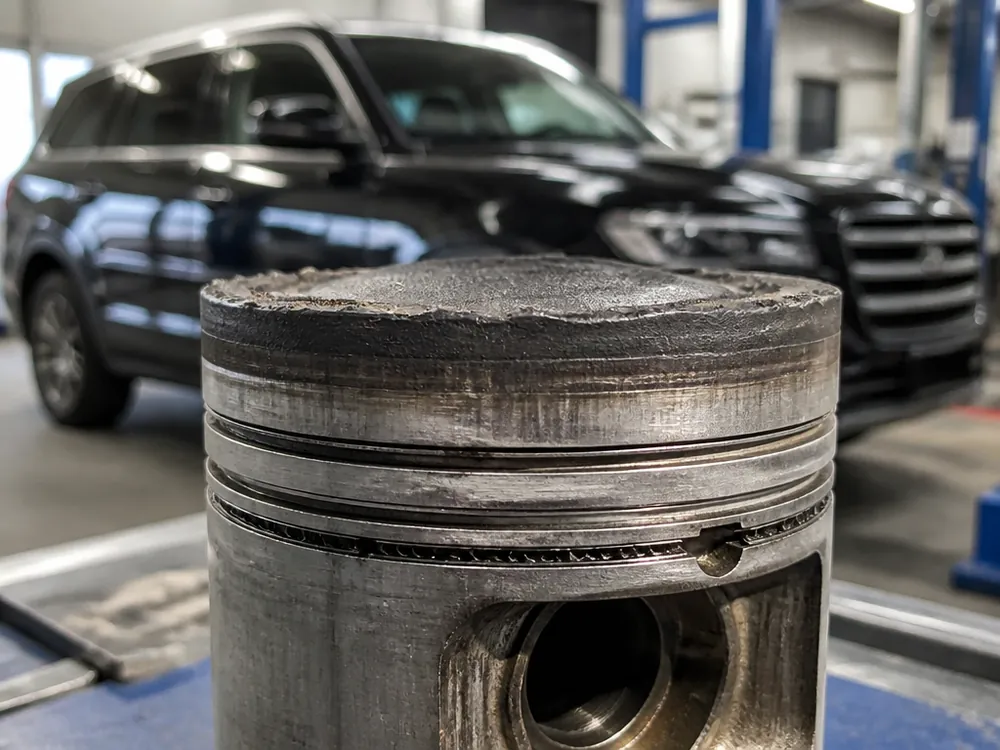
Cylinders: oil consumption, blue smoke from the exhaust and carbon fouling on the plugs usually point to worn walls and rings.
Head: knocking, compression loss in one cylinder and traces of coolant in the oil shift suspicion to the seats and deck.
Measurements: a bore gauge shows the actual cylinder wear in hundredths of a millimeter, pressure testing reveals cracks and leaks.
Conclusion: a symptom without measurements stays a guess, and a measurement report separates a worn unit from a healthy one.
When a cylinder block needs boring
Cylinder block boring in Almaty is needed when wear goes beyond tolerance. We break down the real signs of wear and the measurement figures that decide whether to machine the cylinder bore or get by with new piston rings for now.
Signs it's time to bore the cylinders
Oil consumption: if a noticeable amount disappears between oil changes and there's nothing under the car, that's the first reason to measure the bore.
Blue smoke on warm-up: oil gets into the combustion chamber and burns off — a sign of worn walls or piston rings.
Compression drop: uneven readings across cylinders point to wear or stuck rings.
Knocking under acceleration: a dull sound calls for checking the piston group, not just the bearings.
Oil consumption isn't a verdict: the turbo and valve stem seals cause it too — without a bore gauge you can't conclude that machining is needed.
Which measurements show that machining is needed
Bore gauge by bands: we measure each cylinder at several bands and compare the result with the manufacturer's tolerance.
Ovality and taper: wear beyond tolerance is a direct signal to restore engine geometry, not to "drive it a bit longer."
Manufacturer's tolerance threshold: ovality beyond the manufacturer's tolerance is a reason to remove metal from the wall, otherwise the rings never seat and oil consumption grows.
Choosing the repair size: from the measurement the technician determines which piston to install rather than working by eye.
Control measurement: after the job we issue a report with the actual dimensions of each sleeve.
12-month warranty: the term and conditions are recorded in the work order — for the work performed and the parts installed.
Cylinder block boring, sleeving or block replacement
Depending on the block's condition, one of three paths is chosen: regular cylinder machining, installing sleeves, or replacing the block. We show the limits of each option so you don't agree to unnecessary work.
When boring is enough and when you can't do without sleeving
Boring without sleeves: suitable if cylinder wear fits within the repair sizes and there are no deep scores or cracks on the bore.
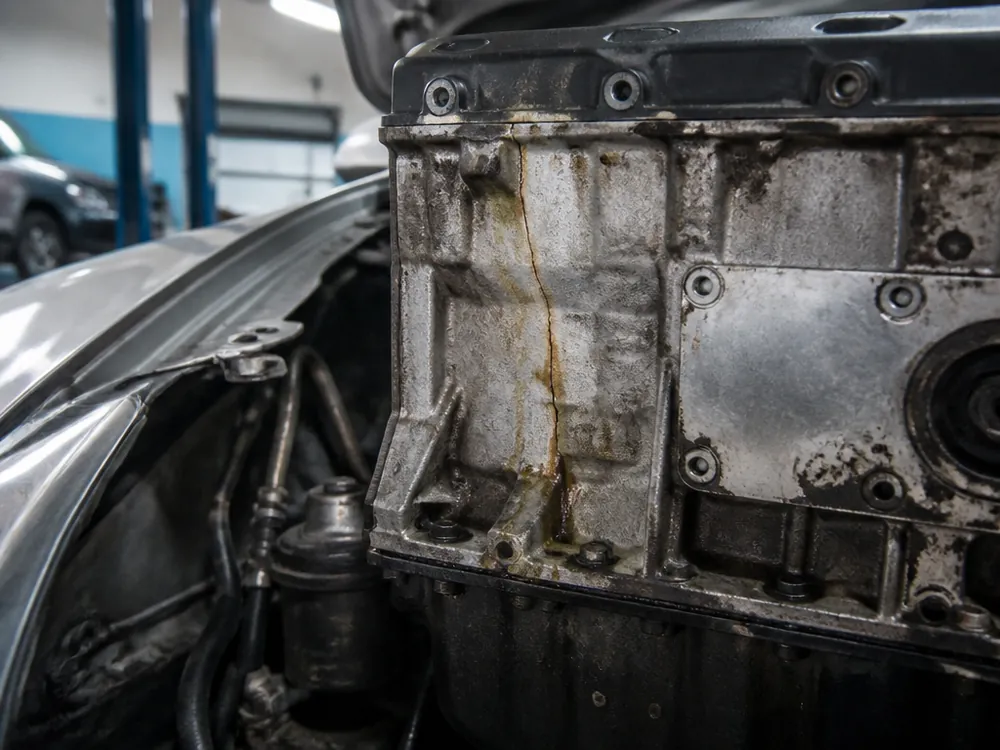
Sleeving: needed for wear beyond the last repair size, deep grooves or a crack in the wall.
Block replacement: the option for when the cooling jacket is damaged or the crankshaft journals can't be restored.
Press-fit interference: we install the sleeve with 0.05 mm interference — otherwise it spins and the whole unit has to be replaced.
Check before work: first a bore gauge measurement and inspection, otherwise it's easy to start machining where a sleeve is already required.
Why an aluminum block is machined differently from a cast iron one
Cast iron body: the cylinder wall is hard enough, so machining goes directly for an oversize piston.
Aluminum body: the wall is soft and you can't remove a layer from it directly — the surface wears fast and scores.
Order of work: first the sleeve is pressed in, and only then is it machined to size and honed.
Question for the technician: how exactly they plan to machine the aluminum — a direct answer about sleeving confirms they understand the technology.
Sign of trouble: a promise to "just bore the aluminum" without a sleeve means the technician isn't accounting for the difference in materials.
Repair sizes and piston selection
A measurement turns a vague "time to bore" into a specific figure accurate to hundredths. We break down how we pin it down before the machine and why you can't machine a cylinder for a part that isn't on the bench yet.
How a measurement becomes a repair size
Measuring with a bore gauge: we measure each cylinder at several heights and planes to spot out-of-round and taper.
Piston selection: based on the results, we take a part of the required repair size — first, second, or third.
Thermal clearance: we bore to the selected part with the manufacturer's clearance, not "by eye."
Fixing the size before machining: we agree on the size with the client and only then put the block on the boring machine.
Post-machining inspection: we recheck the geometry to make sure it matches the calculated spec.
Cost of a mistake: if metal is removed for one size but the piston turns out to be a different size, the part is scrap — that's why we fix the size in advance.
Work options based on block condition
set of works based on block condition
Work option
When we use it
What's included
Boring one cylinder
local wear
measurement, boring, honing
Boring an inline four
wear on all four
measurement, boring, honing
Boring a V6 block
V-type engines
measurement, boring all cylinders
Boring with sleeve installation
deep scoring, cracks
press-fit sleeving, boring, honing
Boring with bearing saddle repair
saddle deformation
runout check, saddle repair
Boring with bearing replacement
bearing wear
bearing replacement, control measurement
Can I bring my own pistons and rings for installation
Your own pistons: we accept them, but first check the size and geometry — we bore the block only after that.
Rings and bearings: we install the client's components if they match the selected size in dimensions and condition.
Parts choice: we work with OEM, aftermarket, or the client's components — the car owner decides what to install.
Old parts: we show and return the removed pistons and rings so it's clear what was replaced.
Warranty: 12 months on the work performed applies to our parts; parts brought by the client are not covered.
How the work is done and why you can't skip honing
We show step by step how engine cylinder boring goes from intake to delivery, and why no stage in this chain can be skipped.
Work stages from intake to delivery
Inspection and measurement: we accept the part, use a bore gauge to measure wear on the cylinders, and record the results in a protocol.
Washing: we wash off carbon deposits and chips, otherwise abrasive will get under the cutter and cause scoring.
Setup and alignment: we align the block on its mounting surfaces before machining.
Machining: we remove metal down to the calculated repair size for the selected piston.
Honing and pressure testing: we apply a hone pattern to the walls and check the water jacket for leaks.
Control measurement: we measure the cylinders again and issue a protocol with actual dimensions.
Photo report: we take pictures at key stages and show and return old parts — so you can see what was actually replaced.
Why honing is needed after cylinder machining
Wall microprofile: the cutter leaves longitudinal grooves, and without a hone pattern oil drains off them.
Oil film retention: intersecting grooves hold lubricant on the cylinder wall and feed it to the ring.
Ring break-in: the right surface roughness lets the ring seat gently against the cylinder.
Geometry control: the hone removes fractions of a micron and corrects out-of-round left by the cutter.
Consequence of skipping: without this operation the rings don't break in, and the engine smokes and burns oil even after "quality" machining.
How to tell a direct contractor from a middleman by the signs
Dedicated engine specialist: we have a separate engine specialist in our shop, and the unit is not handed off to random subcontractors.
Photo report by stages: a middleman usually doesn't show the process, while a direct contractor photographs the inspection and measurement.
Control measurement protocol: a document with actual cylinder dimensions confirms the work was actually done.
Old parts at pickup: if the shop doesn't return the removed pistons and rings, there's no way to verify the scope of work.
Timelines, warranty, and break-in after boring
Repair duration and warranty terms depend on the scope of block work, and break-in affects engine life. We explain how we set timelines, what the warranty covers, and how to behave in the first kilometers.
How long the car stays in the shop
Restoration without removing the block: takes less time than sleeving with saddle repair — we put the exact timeframe in the written estimate after inspection.
Estimate before repair starts: first diagnostics and measurement, then calculation; we start work only after the client agrees.
Urgent work: we do it within a day, but only when the block is already removed and inspection has found no cracks.
Sleeving and saddle repair: add press-fitting sleeves with 0.05 mm interference and inspection, so the timeframe grows compared to simple cylinder boring.
Photo report by stages: we photograph key operations so the client can see which surfaces were machined.
Test drive before pickup: we check the engine on the road and confirm smooth operation.
What the warranty on performed work covers
Warranty period: we give 12 months on cylinder restoration — the same standard as for the engine, cylinder head, and timing belt.
A document, not a promise: we record the period and terms in the work order and the completion certificate when the car is picked up.
Free diagnostics: for a warranty case, we inspect at no charge to immediately understand the cause.
What it covers: the warranty applies to the work performed and the parts we installed.
What it doesn't cover: an accident after repair, third-party interference, natural wear of consumables, and parts brought by the client.
Transparent terms: limitations are written in the certificate in advance — the client sees them before pickup, not when a dispute arises.
How to break in the engine after cylinder restoration
First miles after the repair: keep the RPMs moderate and don't rev the engine to the redline — the rings need time to seat against the fresh hone.
No full load: don't tow a trailer and don't carry heavy loads while break-in is underway.
Oil change after break-in: once it's done, the oil is changed — break-in debris stays in it.
Break-in as a warranty condition: if the engine is loaded right away, the rings don't seat, and oil consumption claims won't be accepted.
Key checks for cylinder boring
We've put together what determines the result of cylinder machining: the right assembly, measurements, repair size, honing and a documented warranty. Below is a short summary you can use to check any shop.
Assembly: machining the block and the cylinder head are different operations, and a competent technician starts by sorting out the symptom, not the name of the service from the ad.
Measurements: the decision to bore is made based on bore gauge readings and a teardown inspection, not on carbon buildup on the walls or a single symptom like smoke from the exhaust.
Material: a cast iron block is machined directly, an aluminum one only with sleeving, and the sleeve is pressed in with about 0.05 mm interference, otherwise it will spin.
Piston group: the repair size and the part itself are fixed before work begins, otherwise the new piston simply won't fit the cylinder.
Finishing: honing is essential for proper lubrication, and demand that the warranty with break-in conditions be written into the work order and the handover report.
11
Frequently asked questions about cylinder block boring in Almaty
Questions.
Price, timeframes, warranty, payment — 10 questions asked most often.
10
Didn't find an answer?
Message us on WhatsApp — a service advisor will reply within 5 minutes.
The cost of cylinder block boring at our auto service CARGID in Almaty starts from 15,000 tenge per cylinder. The final price depends on several factors: cylinder diameter, block material (cast iron or aluminum), the need for sleeving, the complexity of defects (cracks, scoring), as well as the volume of additional work such as honing and washing. The car brand also matters: some engines require special tooling. The exact cost can be quoted after block inspection, which we perform free of charge when you order boring. For example, boring for a classic VAZ will be cheaper than for a Japanese or German engine. We always provide an estimate before starting work so you know all the costs in advance.
The standard turnaround time for cylinder block boring at our service is from 2 to 4 business days. This period includes the boring itself, honing, washing, and control measurements. If sleeving or other additional work is required, the time may increase to 5-7 days. Rush orders are possible for an additional fee, usually 1-2 days. During the work, we can offer a replacement car if you need to get around the city. Exact deadlines are agreed upon when the block is accepted for work and recorded in the contract. We value your time, so we try to complete the work within the agreed deadlines, but sometimes delays are possible due to the delivery of repair pistons or other components.
For cylinder block boring work we provide a warranty of 12 months or 10,000 km of mileage, whichever comes first. The warranty covers the quality of work performed: adherence to dimensions, surface roughness, absence of deformations. If problems related specifically to boring arise during the warranty period, we will fix them free of charge. Important: the warranty is valid provided that the engine break-in recommendations are followed and that quality piston rings and pistons, which you install, are used. We also give recommendations on oil and additives to ensure durability after repair. If manufacturing defects in parts are found, the warranty on them applies in accordance with the manufacturer's warranty.
Yes, an appointment is advisable, as our auto service is often busy. You can book by phone or via messenger, choosing a convenient time. When booking, we will clarify the make and model of the car, as well as the preliminary defects, in order to prepare the necessary equipment. If you come without an appointment, we can only accept your block if there is an available slot, which may require waiting. An appointment guarantees that your block will be accepted at the agreed time, and we will immediately begin inspection. Usually inspection takes about an hour, after which we agree on the scope of work and cost with you. To book, just call us a day or two in advance. We are located in Almaty, at [address], you can book on the website or by phone.
Yes, you can bring your own pistons, rings, bearings, and other components. We will accept them and check compliance with the dimensions after boring. It is important that the pistons are of repair size (usually +0.5 or +1.0 mm), otherwise boring will be pointless. If the pistons are used or defective, we can recommend purchasing new ones from our trusted suppliers, but you are entitled to use your own. In this case, responsibility for the quality of the parts lies with you, but we will perform control measurements and warn you of any mismatch. You can also buy pistons from us — we work with trusted brands and provide a warranty on the parts. The cost of our pistons is comparable to the market, and the quality is confirmed. When using your materials, we reduce the warranty on boring to 12 months, since ring wear may be related to their quality.
If defects related to boring are detected during operation (for example, increased oil consumption, smoke, reduced compression), we will perform diagnostics free of charge. If it is confirmed that the cause is our work, we will fix it at our own expense, usually on the day you come in (complex repairs take up to 3 working days). All work is recorded in the work order with dimensions indicated, and we keep control measurements. If you go to another service and they find problems there, we will conduct an independent examination. It is important to understand that poor boring may not be related to our actions, for example, if unsuitable pistons are installed or break-in is violated. Therefore, we always give detailed break-in instructions and provide further assistance with adjustment. Our reputation is important to us, so we strive to perform work with high precision.
Boring is increasing the cylinder diameter to the repair size and treating the surface to install larger-diameter pistons. Sleeving is replacing a worn or damaged sleeve (insert) in the cylinder block. Most often sleeving is required if the cylinder has deep scoring, cracks, or wear exceeding the permissible repair sizes (usually +1.0 mm). During sleeving, the old sleeve is removed, the seat is bored, and a new sleeve is pressed in, then bored to the required diameter. Sleeving is more complex and more expensive: the cost starts from 25,000 tenge per cylinder plus the cost of the sleeves. Boring is cheaper but has limitations. At our service we perform inspection and will recommend the optimal option. If the wear is minor, boring is sufficient; if the damage is critical, sleeving is needed.
After cylinder block boring, a break-in regime must be followed: for the first 1500-2000 km do not exceed 2500-3000 rpm and do not fully load the engine. It is advisable to drive gently, avoiding sudden accelerations and towing a trailer. Be sure to change the oil and oil filter after break-in, as the oil will contain break-in products. We recommend using quality motor oil with the viscosity specified in the owner's manual. Top up the oil at least once a week and monitor the level. It is also useful to use friction-reducing additives, but in agreement with us. After break-in, be sure to return to our service for a check-up — we will check compression and cylinder condition, and adjust if necessary. Following these recommendations will ensure a long engine life after repair.
We accept payment in cash in tenge, by bank card (Visa, Mastercard, UnionPay), as well as by transfer to an account for legal entities. For individuals, payment is made after the work is completed, once you have accepted the work. Without prepayment we begin inspection, but the boring itself is performed after the estimate is agreed, and you can pay for it upon completion. Installments for auto service are available through our partner bank for amounts from 50,000 tenge for a period of up to 6 months. To arrange an installment plan, only an ID card is required. If you have questions about payment, call us — we will find a convenient option. Payment by QR code via Kaspi or other apps is also possible. We always issue a receipt and warranty card.
The main signs: increased oil consumption (more than 0.5 l per 1000 km), smoke from the exhaust pipe (bluish or white), drop in compression, piston knocking during operation (especially when cold), carbon deposits on the spark plugs. During diagnostics we measure compression and perform endoscopy of the cylinders. If there is scoring on the walls, or ovality or taper exceeding the permissible value (for example, more than 0.05 mm per diameter), then boring is inevitable. Boring is also required when installing repair pistons of repair size. If cracks or deep damage are found, sleeving may be needed. Do not ignore these symptoms, as delaying can lead to piston seizure and a complete engine overhaul, which will cost significantly more. It is better to come to us in advance — we will perform a full block diagnostics for 5000 tenge, with subsequent credit when the work is performed.
12
What clients say after cylinder block boring
Reviews.
We collect ratings on the website and on maps — we hide nothing.
4.8
872 reviews on the website 1 900+ ratings in total
Alexander
They bored the block on my Volkswagen Passat B5. The scoring was terrible, it was guzzling oil by the liter. They did it in 3 days, returned it with new pistons, everything was spot on. I paid 145,000, which is fine for this kind of work. The engine now runs quietly, compression is even in all cylinders. The guys did a great job, explained everything.
Dmitry
CX-5
I brought in a Mazda CX-5 with severe vibration and knocking. Turned out the cylinder ovality was due to overheating. They did the boring and honing, installed a piston assembly. Total was 178,000, took 4 days. The car now drives like new, I can't believe it. Thanks for the honesty and speed!
Yerzhan
My car is a Hyundai Accent, the cylinder surfaces were worn. I had boring done and new pistons installed. Everything was ready in 3 days, I paid 150 thousand tenge. Now the engine runs great, power has increased. Thanks to the craftsmen!
Igor
Toyota Camry
I took a block from a Toyota Camry for boring. They found a crack in the block, but not in the cylinder. They did pinning, bored it, checked everything under pressure. They returned it for 220,000, turnaround 5 days. I was scared, but the result is excellent — the engine is dry, doesn't eat oil. Plus there's a warranty on the work!
Sergey
My Lada Granta had stepped cylinder wear. They bored it to the repair size, installed new pistons with rings. It came to 162,000, done in 3 days. The block was washed, honed properly. The car stopped smoking, acceleration is better. Thanks, now I know where to go!
Azamat
Honestly, I was worried about the quality of boring in Almaty, but they reassured me here. I had the block on a Nissan Qashqai done after an overhaul — it turned out the cylinders were crooked. They rebored it here, restored the geometry. All work came to 195,000, done in 5 days. After a week of break-in — all good. I recommend.
Maxim
The block on a Mercedes W211 had scuffing after a timing belt break. They removed it, bored it, honed it, installed repair pistons. The total was 210,000, turnaround 4 days. Excellent work, everything neat, with measurements done in my presence. The engine purrs like a kitten. Thanks to master Artyom for the detailed explanations!
Andrey
Kia Rio
I came in about boring the block on a Kia Rio. The diagnosis was scoring due to oil starvation. They did everything with quality: boring, honing, replaced the piston assembly. I paid 148,000, waited 3 days. Compression is 13-14 in all cylinders! They work like clockwork. Thanks!
Timur
I needed the boring done accurately and quickly on the block on the address. My Škoda Octavia was consuming oil, the cylinders were heavily warped. They did it in 3 days, price 155,000. The engine is now quiet, it practically doesn't consume oil. Thanks for the professionalism!